| Brand Name: | HongCe |
| Model Number: | HC-EXR1200 |
| MOQ: | 1 Set |
| Price: | Negotiation |
| Payment Terms: | T/T,L/C |
| Supply Ability: | 50 Sets per Month |
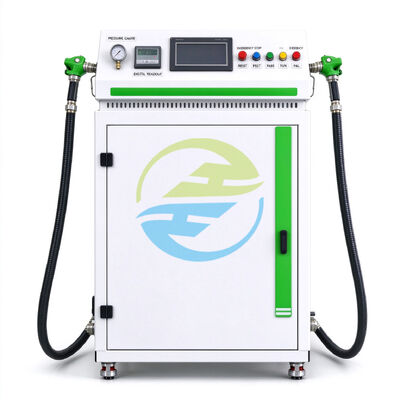
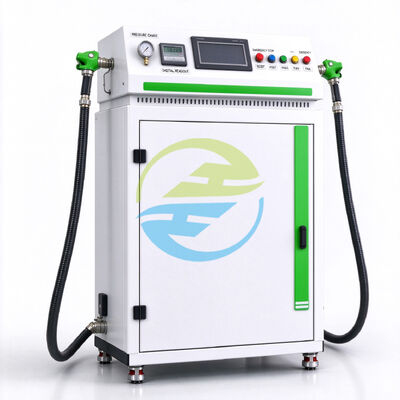
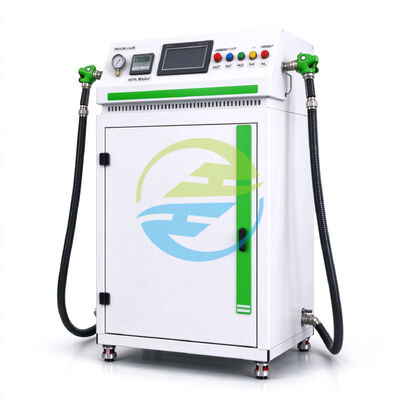
R290 and R32 are efficient refrigerants, but they are also flammable, so a standard recovery unit is not the right tool for them. This recovery machine is built around an explosion proof motor, a sealed spark free electrical enclosure and static grounding connections, so recovery work on A3 and A2L systems can be carried out inside the workshop without adding a temporary hazardous area.
The unit recovers liquid at up to 1.2 kg per minute and vapour at about 0.35 kg per minute through a two stage spark free vacuum pump that reaches 30 microns. Recovered refrigerant is pushed into a 12.5 kg internal cylinder with a level indicator, and weight, pressure and vacuum are shown on a digital display so the technician knows exactly how much has been taken out of the system and when the system is empty.
| Measured item | Range / resolution | How it is measured | What it tells the operator |
|---|---|---|---|
| Recovered refrigerant weight | Digital readout, cylinder scale | Load cell under the internal cylinder | How much refrigerant has been recovered, and how much room is left in the cylinder |
| Recovery rate | Up to 1.2 kg per minute liquid, 0.35 kg per minute vapour | Weight change per unit time | Whether the recovery is progressing normally or the line is restricted |
| Suction and discharge pressure | Digital pressure readout | Pressure sensors on the recovery circuit | Blocked filter, closed valve, cylinder full, over pressure risk |
| Vacuum level and ultimate vacuum | Down to 30 microns | Vacuum sensor on the pump inlet | Whether the system has been emptied to the level required before opening it |
| Automatic cut off point | Preset vacuum or pressure limit | Controller logic with automatic stop | Stops the machine without the operator watching the gauge, which matters on flammable work |
| Cylinder fill level | 12.5 kg cylinder with level indicator | Visual indicator plus weight readout | Prevents overfilling, which is a safety limit for A3 refrigerants |
| Safety device status | Over pressure, thermal cut off, grounding terminal | Hardware protection plus visible grounding point | Confirms the machine is operating inside its safe envelope |
The motor is an Ex d IIB T4 explosion proof type and the electrical compartment is sealed and spark free. In flammable refrigerant work the ignition source is not usually the refrigerant itself but an arc inside a switch or a hot motor surface, so the protection is concentrated where the energy is: the motor, the control box and the wiring entry points.
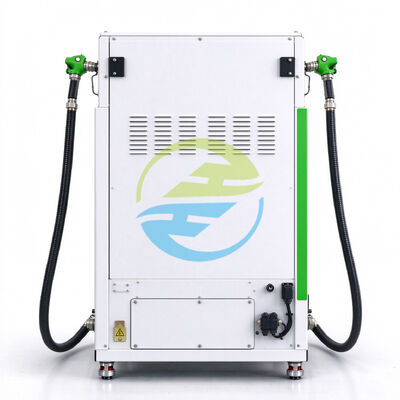
Flowing refrigerant generates static charge, and a hose that cannot dissipate it becomes the ignition risk. The machine has a dedicated grounding terminal and is supplied with anti static recovery hoses and self sealing couplers, so the circuit is bonded from the system being recovered through the machine to the building earth. The grounding point is a deliberate, visible part of the design rather than an afterthought.
The 7.2 CFM two stage pump pulls the system down to 30 microns while the recovery circuit pushes liquid refrigerant out of the system in parallel with vapour recovery. The push pull arrangement is what allows the 1.2 kg per minute liquid rate on larger A2L and A3 charges without asking the pump to handle liquid directly.
Recovery stops automatically at the preset vacuum, and over pressure, thermal cut off and cylinder fill limits work as the second and third layer. On flammable refrigerants this matters because the technician's attention is on the system and the grounding, not on a gauge needle.
| Parameter | Specification |
|---|---|
| Refrigerant types | R290 / R32 (A3 and A2L flammable refrigerants) |
| Ex protection | Ex d IIB T4 explosion proof motor, ATEX compliant design |
| Recovery rate | 1.2 kg per minute liquid, 0.35 kg per minute vapour |
| Vacuum pump | 7.2 CFM two stage, spark free |
| Ultimate vacuum | 30 microns |
| Internal cylinder | 12.5 kg with level indicator |
| Hoses | Anti static recovery hoses with self sealing couplers |
| Display | Digital weight, pressure and vacuum readout |
| Safety devices | Over pressure cut off, thermal cut off, grounding terminal |
| Power supply | 220 V 50/60 Hz |
| Model number | HC-EXR1200 |
| Certification | CE, ATEX, ISO 9001:2015 |
| Place of origin | Guangzhou, Guangdong, China |
| Brand | HongCe |
The machine is used wherever A3 or A2L refrigerant has to be taken out of a system safely, whether for production, service or decommissioning:
Equipment for flammable refrigerant is judged on its safety file as much as its recovery rate, so the documents and the support behind the machine are part of the product.
| Support item | What is provided |
|---|---|
| Warranty | Twelve months on the explosion proof motor, vacuum pump, controller and sensors, extendable on request |
| Safety documents | ATEX documentation and material certificates supplied on request, so the safety file of the workshop can be completed |
| Spare parts | Recommended spare parts list agreed at order stage, including hose sets, couplers, filter driers and seals |
| Emergency support | Service support aimed at 24 hour response for safety related questions, with remote diagnosis by video call |
| Calibration | Annual inspection and calibration service for weight, pressure and vacuum channels with a certificate |
| Training | Operator training material on grounding, hose bonding and cylinder limits supplied with the unit |
| Documentation | English operation manual and wiring diagram with every machine |
The unit is built to ATEX compliant design with an Ex d IIB T4 explosion proof motor and a sealed spark free enclosure, and it is CE marked. ATEX documentation and material certificates are supplied on request. Please send us the zone classification and national requirements of your workshop so our engineers can confirm the configuration against your local rules before the order.
Yes, the recovery circuit is compatible with common A1 refrigerants as well. In practice most customers keep separate hose sets per refrigerant group to avoid mixing, and we supply additional hose sets for that purpose.
The internal cylinder is 12.5 kg and has a level indicator plus a weight readout. For A3 refrigerants the fill limit is set well below the physical capacity, and the machine cuts off automatically. Never rely on the indicator alone: the weight display is the reference.
A residential split contains roughly 0.8 to 1.5 kg of R32, which is recovered in a few minutes in liquid mode once the circuit is pulled down. Actual time depends on line length and whether the refrigerant is recovered as liquid or vapour; vapour recovery is about 0.35 kg per minute.
220 V 50/60 Hz single phase is standard. Other voltages and plug standards are available on request. The supply must be earthed, and the grounding terminal on the machine must be bonded to the building earth before the recovery starts.
The pump oil, filter drier and hose seals are the wear items. A filter drier and spare seal set are supplied with the unit, and we recommend an annual check of the pressure and vacuum channels together with the grounding continuity, which can be combined with the calibration service.
The recovery unit, an anti static hose set with self sealing couplers, a grounding cable set, a spare filter drier, an English operation manual and export plywood packing. ATEX documentation is added on request.
| Aspect | HongCe explosion proof recovery machine | Typical low cost alternative |
|---|---|---|
| Motor and enclosure | Ex d IIB T4 explosion proof motor with sealed spark free electrical box | Standard motor in an open frame, no ignition protection |
| Intended refrigerants | Explicitly designed for A3 and A2L, including R290 and R32 | Marketed for "all refrigerants", with no A3 provision |
| Static control | Grounding terminal plus anti static hoses supplied as standard | No grounding point, ordinary hoses |
| Recovery rate | 1.2 kg per minute liquid through a two stage 7.2 CFM spark free pump | Single stage pump, liquid recovery through the vapour port |
| Stopping | Automatic cut off at preset vacuum with over pressure and thermal protection | Manual stop, operator watches the gauge |
| Documentation | CE, ATEX design documents and material certificates on request, ISO 9001:2015 production | Manual only, certificates difficult to obtain |
| Safety support | Guidance on zone classification, grounding and cylinder limits from the design team | No process or safety guidance |
| Advantage | What it means for your project |
|---|---|
| Manufacturer, not an assembler | Refrigerant and electrical test equipment has been made in our Guangzhou workshop since 2003, not assembled from third party kits |
| One safety concept | Explosion protection is designed together with the refrigerant circuit, so motor, enclosure, grounding and hoses form a single system |
| Documents for the safety file | ISO 9001:2015 production, CE marked machines and ATEX design documentation available for workshop audits |
| Flammable refrigerant experience | Around half of annual output is exported, including customers working with A3 and A2L refrigerants in series production |
| Own pump and sensor technology | Two stage spark free pump and push pull recovery designed in house, with a short parts and service loop |
| Direct engineering access | Zone classification, grounding and cylinder limit questions go to the engineers who designed the machine |
Guangzhou HongCe Equipment Co., Ltd. has been designing and building test and production equipment in Guangzhou, China since 2003. Roughly half of our annual output is exported, and the machines are used by third-party laboratories, appliance and HVAC factories, and inspection bodies that work to IEC, UL, GB and EN standards. Our slogan states the position we have kept for more than twenty years: industry leading test equipment, advanced online systems and solutions, anywhere in the world.
The company is ISO 9001:2015 certified, and machines supplied to the EU market carry CE marking. Mechanical fabrication, control cabinet assembly, PLC and HMI programming, refrigerant circuit assembly and final calibration are all done in our own workshop, so a station can be engineered around a customer's production sequence instead of being adapted from a catalogue item. Our engineers keep the refrigerant, pressure and vacuum know-how in-house, which is why questions about charging recipes, leak limits or flammable refrigerant handling are answered by the people who built the machine.
Flammable refrigerant projects are quoted with the grounding, hose and documentation requirements written into the offer, because those are the parts that a safety audit will ask about later.
Company profile: about us · factory and workshop · quality control · all refrigerant filling equipment · technical news
Customers comparing this machine usually also look at the following stations from our refrigerant filling equipment range:
Send us the refrigerant, the typical charge per system, the number of systems recovered per day and the zone classification of your workshop, and our engineers will confirm the machine configuration, the documentation package and the delivery time. The rest of our refrigerant filling equipment range is listed on the products page, and you can contact our sales engineers directly for flammable refrigerant projects.