logo

products details

Created with Pixso. Home Created with Pixso. Products Created with Pixso.
Helium Leak Testing Equipment
Created with Pixso.

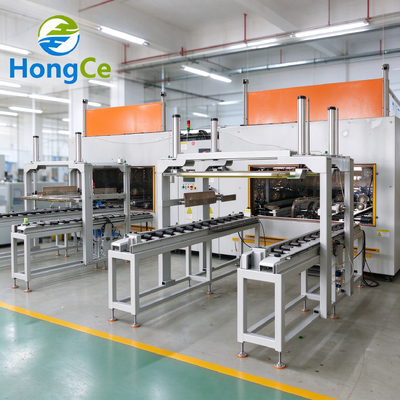
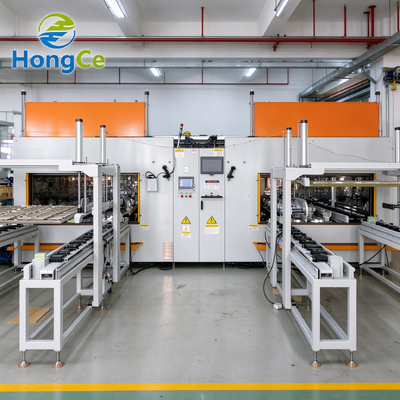
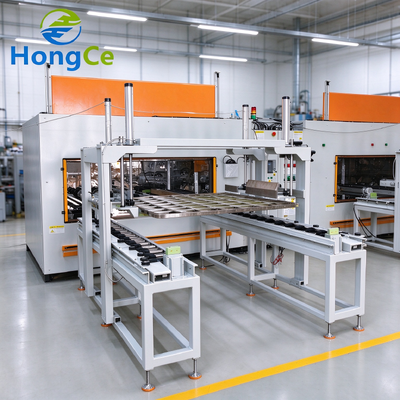
Helium Accumulation Chamber Leak Test Equipment 1.0E-6 Mbar.L/S For EV Battery Pack Hood Method Detection

Helium Accumulation Chamber Leak Test Equipment 1.0E-6 Mbar.L/S For EV Battery Pack Hood Method Detection

Brand Name: HongCe
Model Number: HJ209
MOQ: 1 Set
Price: Negotiation
Payment Terms: T/T,L/C
Supply Ability: 1 set per 3 months
Detail Information
Place of Origin:
Guangdong, China
Certification:
Third-party certification certificate(cost additional)
Minimum Detectable Leak:
1.0E-6 Mbar.L/s
Helium Concentration:
10% - 100%
Helium Recovery Rate:
≥90%
Hood Size:
1200 X 800 X 400 Mm
Cycle Time:
6 - 10 Min Per Pack
Power Supply:
AC 380 V, 3-phase, 15 KW
Compressed Air:
0.6 MPa Dry, Oil-free
Weight:
2200 Kg
Packaging Details:
Skid-mounted frame, hood openings sealed with desiccant bags, sea-worthy plywood enclosure with ISPM-15 marking
Highlight:

Accumulation Hood Leak Testing

,

EV Battery Pack Airtightness

,

Tracer Gas Concentration Measurement

Product Description

A finished battery pack cannot be evacuated, cannot be wetted, and cannot be inspected seam by seam within a takt. The hood method is the only one of the three that keeps the pack dry, gives you a number, and fits a production shift — which is why this is the system we build for pack-level sealing verification.

Is This Machine the Right Purchase for You?
This machine is the right purchase if:
  • You assemble or seal battery packs, modules, or energy storage enclosures.
  • Your requirement is IP67 or IP6K9K, or a coolant-loop sealing criterion your customer will audit.
  • You need a per-pack record, not a sampling statistic.
  • You already know a vacuum chamber is not an option for a completed pack.
Look elsewhere if:
  • Your packs are small enough to evacuate and you have the volume — a chamber is faster and more sensitive.
  • You need to find a leak on returns rather than prove a seal on production — that is a probe job.
  • Your acceptance criterion is gross only, and an air decay test already passes audit.
Why a Pack Breaks the Usual Rules

Every leak testing method assumes something about the part. Vacuum chamber testing assumes the part can be evacuated, and a pack cannot — the cells, the structural foam, and the seals are not designed for external vacuum, and pulling one down will damage it or, worse, deform it in a way that creates the leak you were testing for.

Water immersion assumes you can dry the part afterwards. On a high-voltage assembly, that assumption is unacceptable, and it leaves no record you can show a customer.

Air decay assumes a small, stiff, temperature-stable volume. A pack is the opposite: tens of litres, a lot of thermal mass, and an acceptance criterion that is usually far below what air can resolve in a shift, let alone a takt.

The hood method sidesteps all three. The pack stays at ambient pressure, stays dry, and the measurement is a tracer gas concentration rather than a pressure difference — so the material and the volume stop fighting the test.

How It Works, and Where the Sensitivity Comes From

The pack goes into a sealed hood of known volume and is charged with a helium mixture through its service port. Anything that escapes accumulates in the hood. A circulation fan mixes the hood atmosphere so there are no dead zones, and a mass spectrometer samples that atmosphere and measures the rise over a fixed window.

The key point, and the one that decides your cycle time: sensitivity is governed by accumulation time, not by the analyser alone. Doubling the dwell roughly doubles the signal. There is always a trade between the two, and it should be your trade — we will tell you the shortest dwell that honestly meets your criterion instead of quoting a sensitivity number in isolation.

Two practical details make the difference between a stable result and an argument. First, the hood atmosphere is monitored between cycles: a workshop where a cylinder has been venting will otherwise drift the readings all morning. Second, the hood and the pack are both recovered, because on a large volume the pack itself holds most of the gas.

Design Choices and the Reasons Behind Them
Hood volume kept small relative to the pack

A hood that is much larger than the pack dilutes the signal and buys you nothing. We size the hood to the pack envelope with enough clearance for loading, not to a round number.

Mixing, not just waiting

Helium is light and will stratify. Without a fan and a baffle arrangement, the sample point reads whatever is local to it. Our hoods circulate and were checked for dead zones during commissioning, not assumed.

Background monitoring between cycles

Ambient helium compensation is not a nice-to-have on a pack line; it is the difference between a usable limit and a permanent argument with your quality team.

Recovery from hood and pack

Both are evacuated back through the recovery loop after the measurement. Without that, a large-volume pack vents its whole charge every cycle and the running cost quietly becomes the biggest number in the business case.

A recipe per pack, not a recipe per machine

Pack volume, charge pressure, and dwell all change with the product. Recipes are selected by barcode so nobody edits parameters at the station.

How a Cycle Runs
  1. Load and seal — pack into the hood, lid closed and sealed, barcode scanned, service port connected.
  2. Background check — the hood atmosphere is sampled before charging; if ambient helium is too high, the cycle waits rather than producing a false fail.
  3. Charge the pack — helium mixture to the agreed pressure through the service port.
  4. Accumulate — fan circulation for the recipe dwell; the analyser logs the concentration rise.
  5. Measure and convert — the rise is integrated and converted to a leak rate in mbar·L/s, then compared with the limit.
  6. Recover and release — hood and pack recovered, lid opened, pack released with a verdict and a stored record.
Technical Parameters
Item Specification
MethodAccumulation hood with mass spectrometer measurement
Hood sizes1200 × 800 × 400 mm standard; 2000 × 1500 × 400 mm and larger on request
Minimum detectable leak1.0×10-6 mbar·L/s, dependent on accumulation time
Typical cycle time6 – 10 min per pack including charge, dwell, and recovery
Helium concentration10% – 100%; 10% or 20% mixture commonly used
MixingInternal circulation fan with baffle design, dead zones checked at commissioning
Background controlAmbient helium monitoring with automatic compensation between cycles
Helium recovery≥90% from hood and pack, integrated recovery and purification
ControlPLC with 15-inch HMI, 100 recipes, multi-level access
TraceabilityBarcode scan, per-pack record, MES upload over Ethernet
CalibrationAutomatic sequence with calibrated leak, 12-month interval
Power supplyAC 380 V, 3-phase, 50/60 Hz, 15 kW
Compressed air0.6 MPa dry, oil-free
WeightAbout 2200 kg
What It Finds
Test Item Typical Defect What the Customer Sees
Pack housing weld seamsPorosity, incomplete penetration, spatter-induced lack of fusionWater ingress, isolation fault
Sealant and adhesive beadsGaps, insufficient compression, cure voidsMoisture in the pack after a wash
Service cover gasketsUnder-torque, twisted gasket, damaged lipCondensation on the cover
Connector feed-throughsSeal damage during assembly, pin cavity leaksCorrosion at the connector
Coolant port jointsThread and O-ring defectsCoolant loss, pressure fault codes
Pressure relief and vent valvesSeat leakage, wrong cracking pressureFogging or pressure imbalance
Module interfacesLeaks between sub-assembliesHard to trace later — which is the point of testing now
Setting the Limit, and Tying It to IP

Pack customers usually arrive with an IP67 or IP6K9K requirement and no leak rate, and expect a conversion table. There is no universal one, because it depends on pack volume and on the pressure profile the standard applies. What works is an empirical correlation on your own packs:

  • Test known-good packs and record the spread. That establishes what normal looks like on your line.
  • Introduce a calibrated leak at a known location and confirm the hood sees it at the dwell you plan to run.
  • Set the limit with margin — typically one third of the specified rate — so a marginal pack is caught before the vehicle plant does.
  • Revalidate after a design change. A new pack volume changes the conversion; do not inherit the old limit.

Hood testing measures the whole pack, so it tells you that something leaks, not which seam. Keep a portable sniffer at the rework bench: a two-minute sweep on the suspect area usually identifies the joint, and that is far cheaper than scrapping or reworking blind.

Compared With the Alternatives
Method Sensitivity Pack Wetted Cycle Operator Dependence
Accumulation hood, this machine1×10-6 mbar·L/sNo6–10 minLow
Vacuum chamber1×10-9 mbar·L/sNoNot feasible on a finished packLow
Air pressure decayAbout 1×10⁻³ mbar·L/sNo10–30 min at pack volumeMedium
Water immersion or bubbleGross leaks onlyYes5–15 minHigh
Helium sniffer spray1×10-7 mbar·L/sNo5–20 minHigh

If the pack design allows evacuation, a vacuum chamber is faster and more sensitive and you should buy one. It is the sealed pack with a large internal volume that makes the hood the practical answer — and that describes almost every finished pack we have been asked about.

Frequently Asked Questions
Why can a finished pack not go into a vacuum chamber?

Because the chamber method requires evacuating the part. A pack is not designed for external vacuum: cells, structural elements, and seals can be damaged, and any deformation invalidates the test. The hood keeps the pack at ambient pressure and measures what leaks out instead.

How long does a test take, and can we make it shorter?

Six to ten minutes is typical. Shortening the dwell raises the minimum detectable leak, because the signal grows with accumulation time. Give us the acceptance criterion and we will give you the shortest dwell that still meets it honestly.

What helium mixture should we run?

Ten or twenty percent in nitrogen is common for packs: it keeps cost and supply risk down and is safe to handle. The controller compensates for concentration, so results stay comparable between mixtures.

Will helium in the workshop cause false failures?

It can, which is why the hood monitors ambient helium between cycles and pauses if the background is too high. Keep cylinder venting away from the station, and give the area a few minutes after a burst hose — same discipline as any tracer gas installation.

Can the hood be integrated into a conveyor line?

Yes. Roller or chain conveyor through the hood, automatic lid actuation, and a handshake with the line PLC are standard options. Most customers start with manual loading and automate the second line.

What happens to the helium after the test?

The hood and the pack are both drawn through the recovery and purification loop and returned to the buffer tank. On a pack the pack itself holds most of the charge, so recovering only the hood would be a false economy.

Does it test the coolant circuit separately?

The hood measures the whole sealed envelope, so a coolant port leak will show. If you need the circuit isolated and tested at higher pressure, we can add a dedicated circuit and a second recipe — say so at the enquiry stage, because it changes the fixture.

What do you need from us to quote?

Pack envelope, internal volume, service port details, target leak rate or IP requirement, and the takt you need to hit. With those five numbers we can size the hood and give you a cycle time rather than a range.

About Guangzhou HongCe Equipment Co., Ltd.

A finished battery pack is the least cooperative object in leak testing: too large to evacuate, too valuable to wet, and too tightly specified for air decay. That constraint is what shaped the machine we build.

HongCe has been making test equipment in Guangzhou since 2012 — 100 to 200 people, about half of production exported, customers that include third-party laboratories and certification bodies. Our three families are IEC and EN safety apparatus, IP ingress equipment and environmental chambers, and leak detection spanning helium chambers, sniffer units, hoods, and recovery.

Hood work is where those disciplines meet: gas handling, an enclosure that opens a hundred times a shift, background monitoring that keeps a workshop's stray helium out of the verdict, and a recovery loop sized for the whole pack rather than for the hood alone.

Every system is leak-checked against a calibrated standard and recorded under its serial number before shipment, commissioned on site with correlation runs on your own packs, and supported from Guangzhou with spares dispatched within 48 hours.

Send the pack envelope, the internal volume, the service port details, and your target leak rate or IP requirement. We will size the hood, estimate helium consumption per pack, and quote a cycle time that matches your takt — not a range to argue about later.